8 Pre-Start Checks for a Solventless Laminating Machine You Should Never Skip
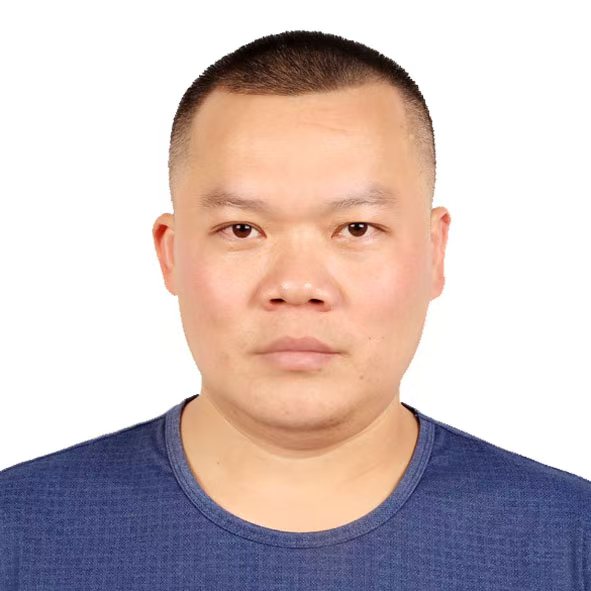
Starting a solventless laminating machine without checking it first may seem like a way to save a few minutes. In practice, it can lead to much bigger problems once production gets underway. Tunneling, uneven coating, unstable web tension, poor bonding, and winding problems can all show up after the machine starts running. By then, you may already have wasted substrate, adhesive, and production time.
A pre-start check does not have to take long. A few basic checks can help catch potential problems before they affect the first roll. The important thing is to follow the same routine each time, rather than checking only when something goes wrong.
For operators and production supervisors, the following eight checks cover the main areas to look at before starting a solventless laminating machine. They are based on common operating conditions and Sinstar’s experience with solventless lamination equipment. With nearly 20 years in the industry and more than 2,680 machines in operation, Sinstar has worked with a wide range of laminating applications and production requirements.
1. Check the Machine and Safety Devices
Start with the machine itself. Check that the emergency-stop buttons, safety guards, sensors and other safety devices are in their normal position and working correctly.
Also look around the machine for loose tools, adhesive residue, material scraps or anything that could interfere with moving parts.
This check is easy to overlook when the machine ran normally on the previous shift. However, a problem with a safety device can stop production immediately after startup or create a safety risk.
Check before starting:
- Emergency-stop buttons
- Safety guards and doors
- Photoelectric or proximity sensors
- Abnormal noise, leakage or loose components
2. Check the Adhesive Supply System
The adhesive system deserves particular attention because changes in adhesive condition can quickly affect coating and bonding.
Before production, check the adhesive temperature, mixing ratio, viscosity and supply condition. Make sure the adhesive lines are clear and check whether there is any cured adhesive, blockage or visible air in the system.
Do not simply assume that the settings from the previous job are still suitable. Different adhesives and material combinations may require different conditions. Some solventless polyurethane adhesives also rely on moisture curing, so the adhesive manufacturer’s technical data should always be followed.
Check before starting:
- Adhesive temperature
- Mixing ratio
- Viscosity
- Glue level
- Pipes and filters
- Signs of blockage or bubbles
3. Inspect the Coating and Metering Rollers
The coating section directly affects adhesive distribution. Before starting, check whether the coating and metering rollers are clean and free from scratches, dried adhesive or other contamination.
The roller gap and pressure should also match the production settings. If the mechanical condition changes, simply entering the correct coating-weight value on the HMI may not be enough.
For high-precision solventless lamination, roller condition, metering gap, roller speed, temperature and adhesive viscosity all work together to determine the actual coating weight.
A small problem at this stage may later appear as uneven coating, unstable bonding or excessive adhesive consumption.
4. Check the Web Tension System
Tension is one of the first things to check when trying to prevent tunneling and other lamination defects.
Check the unwind tension, intermediate tension, lamination tension and rewind tension. Make sure the tension sensors, air shafts, brakes or servo motors are functioning normally.
Do not look only at the number shown on the control screen. The relationship between different tension zones is also important, particularly when combining films with different mechanical properties. Sinstar’s technical guidance notes that stable tension matching is important for maintaining proper alignment between the two substrates.
Watch for:
- Sudden tension fluctuations
- Unstable sensor readings
- Incorrect tension settings
- Film stretching or wrinkles
- Abnormal unwind or rewind movement
5. Check the Substrates and Web Path
Next, inspect the material that will actually enter the machine.
Check the film roll for damaged edges, uneven ends, contamination or telescoping. Make sure the substrate surface is clean and that the required surface treatment, such as corona treatment, meets the production requirements.
Then check the entire web path. The material should pass through the guide rollers correctly without folds, scratches or unnecessary resistance.
This is particularly important when running thin PE film, aluminum foil or other materials that are more sensitive to tension and handling conditions.
A material problem can sometimes look like a machine problem, so it is worth checking the substrate before changing machine parameters.
6. Check the Laminating Nip and Temperature
Before production begins, check the laminating rollers for contamination or damage. Confirm that the roller temperature has reached the required operating condition and that the nip pressure is set correctly.
Temperature and pressure should not be treated as isolated settings. They work together with adhesive properties, coating weight, line speed and substrate condition to determine the final laminate quality.
If the roller has not reached a stable temperature, starting production immediately may produce unstable results during the first few meters or rolls. Give the machine enough time to reach its normal operating condition before judging the process.
7. Check the Rewinding System
A good laminate can still become a problem if the finished roll is not wound correctly.
Before starting, check the rewind tension, contact roller pressure, edge alignment and web guiding system. Make sure the core is correctly installed and that the winding settings match the material being produced.
Pay particular attention to taper tension. As the roll diameter increases, the winding conditions change. Proper taper control helps maintain a stable roll structure and reduce problems such as loose winding, wrinkles or uneven roll edges.
For long production runs, automatic or adaptive taper control can reduce the amount of manual adjustment required.
8. Run the Machine Slowly Before Full Production
The final step is a short test run.
Instead of immediately moving to full production speed, run the machine at low speed for a few minutes. Watch the tension values, adhesive supply, roller movement, motor load, web alignment and rewinding condition.
Listen for unusual sounds and check whether the film is tracking correctly. If something looks abnormal, stop and investigate before increasing the speed.
On machines equipped with digital controls or remote monitoring, production parameters can also be checked through the control system. Some Sinstar models provide closed-loop tension control, automatic adhesive control and remote IoT support for monitoring machine conditions.
The purpose of this step is simple: find a problem while the machine is still running slowly, rather than after a full roll of material has become defective.
What About the First 30 Minutes of Production?
Passing the pre-start inspection does not mean the job can be left unattended.
During the first 30 minutes, pay particular attention to coating weight, web tension, bonding appearance, roll edges and the finished winding condition. If a problem appears, avoid changing several parameters at the same time. Record what changed and adjust one factor at a time where possible.
For example, if tunneling appears, check the actual tension relationship and coating condition before immediately increasing nip pressure. Tunneling can have several causes, including tension, coating distribution, winding conditions and mechanical alignment.
A Simple Pre-Start Habit Makes a Difference
The eight checks above are simple, but they are worth making part of the normal startup routine:
Safety → Adhesive → Coating rollers → Tension → Substrate → Laminating nip → Rewinding → Slow test run
The settings will not be exactly the same for every machine or every job. Adhesive type, substrate combination, laminate structure, and production requirements can all affect the setup. Operators should therefore use the machine manual and the adhesive supplier’s technical requirements as the main reference.
At Sinstar, we also focus on making these routine checks easier to manage through machine design and control systems. Depending on the model, our solventless laminating machines can be equipped with features such as automatic adhesive ratio control, closed-loop tension control, digital parameter management, and IoT monitoring. These functions help operators keep important production parameters under control, but they do not replace a basic inspection before startup.Taking a few minutes to check the machine is usually much easier than stopping the line later to find out why the coating is unstable, tunneling has appeared, or a finished roll has to be rejected. A consistent pre-start routine, together with the right machine settings and operating procedures, can prevent many of these problems before production gets too far.